 MetalsAlloy
380.0 Cast Aluminum
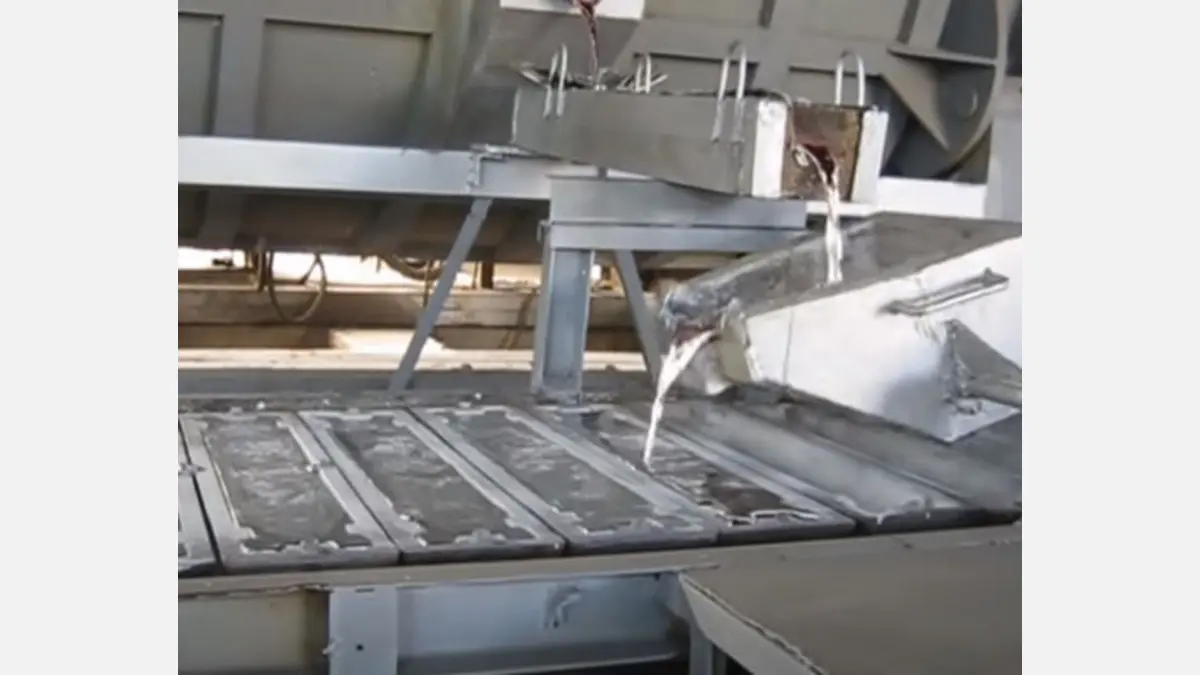
Image Credit: alalloycasting.com
380.0 is an aluminum-silicon-copper casting alloy widely used for pressure die casting where complex shapes, thin walls, dimensional repeatability and economical high-volume production are important. Its 7.5–9.5% silicon content promotes fluidity and castability, while copper contributes to as-cast strength. The alloy is commonly supplied in the F (as-fabricated/as-cast) condition for die-cast components. Compared with lower-copper Al-Si casting alloys, 380.0 offers useful strength and production performance, but its copper-containing chemistry requires attention to corrosion protection and limits its suitability for welding and post-cast heat treatment.
| Chemical Composition wt.% | ||
|---|---|---|
| Element | Min | Max |
| Silicon, Si | 7.5 | 9.5 |
| Iron, Fe | — | 2.0 |
| Copper, Cu | 3.0 | 4.0 |
| Manganese, Mn | — | 0.50 |
| Magnesium, Mg | — | 0.10 |
| Nickel, Ni | — | 0.50 |
| Zinc, Zn | — | 3.0 |
| Tin, Sn | — | 0.35 |
| Other elements, total | — | 0.50 |
| Aluminum, Al | Remainder | |
Registered composition limits for 380.0 die castings, wt.%, from the Aluminum Association Pink Sheets (2025). Single upper limits are shown in the Max column; aluminum is the remainder.
Values below are reported for 380.0-F die-cast material where stated. Actual properties vary with section thickness, die design, casting soundness, local porosity and test method.
Use the button to switch between Metric and US Customary units.
| Physical Properties | Metric |
|---|---|
| Density | 2.76 g/cm³2.76 g/cm³ |
| Mechanical Properties | Metric |
| Tensile Strength | 46,000 psi |
| Brinell Hardness | 80 HB |
| Yield Strength | 159 MPa |
| Elongation at Break | 2.50 % |
| Elastic Modulus | 71.0 GPa |
| Poisson’s Ratio | 0.330 |
| Shear Modulus | 26.5 GPa |
| Shear Strength | 195 MPa |
| Thermal Properties | Metric |
| Linear Thermal Expansion (20–100 °C) | 21.2 µm/m-°C |
| Linear Thermal Expansion (20–300 °C) | 22.5 µm/m-°C |
| Specific Heat Capacity | 963 J/(kg·K) |
| Thermal Conductivity | 109 W/(m·K) |
| Melting Range | 538–593 °C |
| Electrical Properties | Metric |
| Electrical Resistivity | 6.40e-8 Ω·m |
Test conditions & data notes
- Density: 380.0-F die-cast alloy; reported typical value.
- Tensile Strength: 380.0-F die-cast alloy; reported value.
- Brinell Hardness: reported datasheet value.
- Yield Strength: 0.2% offset.
- Elongation at Break: in 50 mm.
- Elastic Modulus: tension.
- Poisson’s Ratio: reported datasheet value.
- Shear Modulus: reported datasheet value.
- Shear Strength: reported datasheet value.
- Specific Heat Capacity: reported datasheet value.
- Thermal Conductivity: reported datasheet value.
- Melting Range: reported datasheet value.
- Electrical Resistivity: Reported as 0.00000640 ohm-cm; test temperature not specified.
Material Conditions & Tempers
380.0 die castings are generally used in the F condition, meaning as fabricated/as cast. Pressure-die-cast 380.0 is normally selected for its as-cast performance rather than for response to a solution-and-aging heat-treatment temper. Component properties should therefore be specified for the actual casting process and critical section thickness.
F: As-fabricated/as-cast condition for die-cast 380.0. Reported values apply to 380.0-F die-cast material; yield strength uses a 0.2% offset.
Advantages & Limitations
| Advantages | Limitations |
|---|---|
|
|
Processing & Fabrication
| Process | Description |
|---|---|
| Pressure die casting | 380.0 is particularly suited to high-pressure die casting. Design gates, runners, vents and overflow locations to fill thin sections rapidly while controlling air entrapment and shrinkage porosity. |
| Machining | Machine only where functional surfaces, threads or sealing features require it. Use casting design to minimize stock removal, particularly near thin walls and areas susceptible to porosity. |
| Joining | Avoid relying on fusion welds for critical load paths or pressure boundaries without procedure qualification. Mechanical fastening, inserts, adhesive bonding or purpose-designed joining features are often more practical for die-cast 380.0. |
| Surface finishing | Apply a finish appropriate to the service environment, such as conversion coating, paint or plating. Preparation must account for the copper- and silicon-bearing die-cast surface and any exposed machining. |
| Die-casting temperature | Reported process range: 635–704 °C (1175–1300 °F). This is a casting process parameter, distinct from the material melting range. Source: https://www.scribd.com/document/549057150/A-380-0 |
Applications
380.0 is used where die-casting productivity and shape capability are central to component value. It is especially appropriate for medium- to high-volume parts that integrate ribs, bosses, mounting points, heat-dissipating features and cosmetic external surfaces in a single casting.
- Automotive housings and brackets: Its die-casting fluidity and useful as-cast tensile strength support compact housings, transmission-related covers, mounts and accessory brackets.
- Electrical and electronic enclosures: Complex, thin-wall enclosures can be produced efficiently with integral ribs, bosses and fastening details.
- Appliance and consumer-product components: High-volume pressure die casting enables repeatable parts with integrated functional features and limited secondary machining.
- Power-tool and equipment housings: The alloy supports robust, shape-intensive housings and covers where weight reduction versus ferrous castings is beneficial.
- General industrial covers and hardware: 380.0 is a practical die-cast choice for parts needing dimensional repeatability, threaded features or machined sealing and mounting surfaces.
Standards & Designations
| Designation | Value | Description |
|---|---|---|
| Aluminum Association | 380.0 | Registered casting/ingot alloy designation listed in the Aluminum Association Pink Sheets publication. |
| Aluminum Association | AA 380.0 | Common reference designation for the 380.0 cast aluminum alloy; the material identity should remain distinct from A380.0. |
Frequently Asked Questions
Is 380.0 the same alloy as A380.0?
No. The 380.0 and A380.0 designations identify different Aluminum Association alloy designations and should not be treated as automatically interchangeable. Purchase orders, specifications and qualification records should state the required designation exactly.
Why is 380.0 widely used for pressure die casting?
Its reported 7.5–9.5% silicon content supports fluid filling of dies, while its 3.0–4.0% copper content contributes useful as-cast strength. This combination is valuable for high-volume components with thin walls, ribs, bosses and other integrated details.
Can 380.0 die castings be welded?
Welding can be challenging because pressure die castings may contain entrapped gas and porosity, which can cause weld defects. For critical joints, use a qualified procedure and verify weld quality; mechanical fastening or purpose-designed joining methods are often preferred.
References & Data Notes
- (n.d.). Aluminum Association, Designations and Chemical Composition Limits for Aluminum Alloys in the Form of Castings and Ingot (Pink Sheets), revised August 2025. https://www.aluminum.org/sites/default/files/2025-10/Pink%20Sheets%202025.pdf
- (n.d.). Aluminum 380.0-F Die Casting Properties. https://www.scribd.com/document/549057150/A-380-0
Composition limits are from the Aluminum Association Pink Sheets (2025). Property values are reported for 380.0-F die-cast material in the cited datasheet; actual casting properties depend on process, section thickness and soundness. Confirm applicable specifications for design or procurement.